In the manufacturing sector, ensuring worker safety is not just important—it’s vital. From busy assembly lines to high-risk areas, adhering to safety standards is fundamental for creating a productive and secure work environment. However, conventional methods of monitoring Personal Protective Equipment (PPE) compliance often suffer from inaccuracies and inefficiencies.
AI-powered PPE monitoring is revolutionising this process by utilising advanced computer vision and deep learning to automate and improve safety practices. This technology guarantees that workers on the factory floor are consistently protected, minimising accidents and ensuring compliance with regulations.
Why PPE Monitoring is Critical in Manufacturing
Industries encounter various challenges regarding safety
High Risk of Injuries and Accidents: Ignoring PPE protocols can lead to avoidable accidents, disrupting operations and putting lives at risk.
Hazardous Exposure: Not wearing the correct PPE can expose workers to dangerous chemicals, extreme conditions, or mechanical threats.
Regulatory Compliance: Failing to follow safety regulations can result in significant fines and damage to a company’s reputation.
AI-powered PPE monitoring effectively tackles these issues, providing manufacturers with a dependable and scalable solution to uphold workplace safety.
How AI-Powered PPE Monitoring Works
- Computer Vision Technology
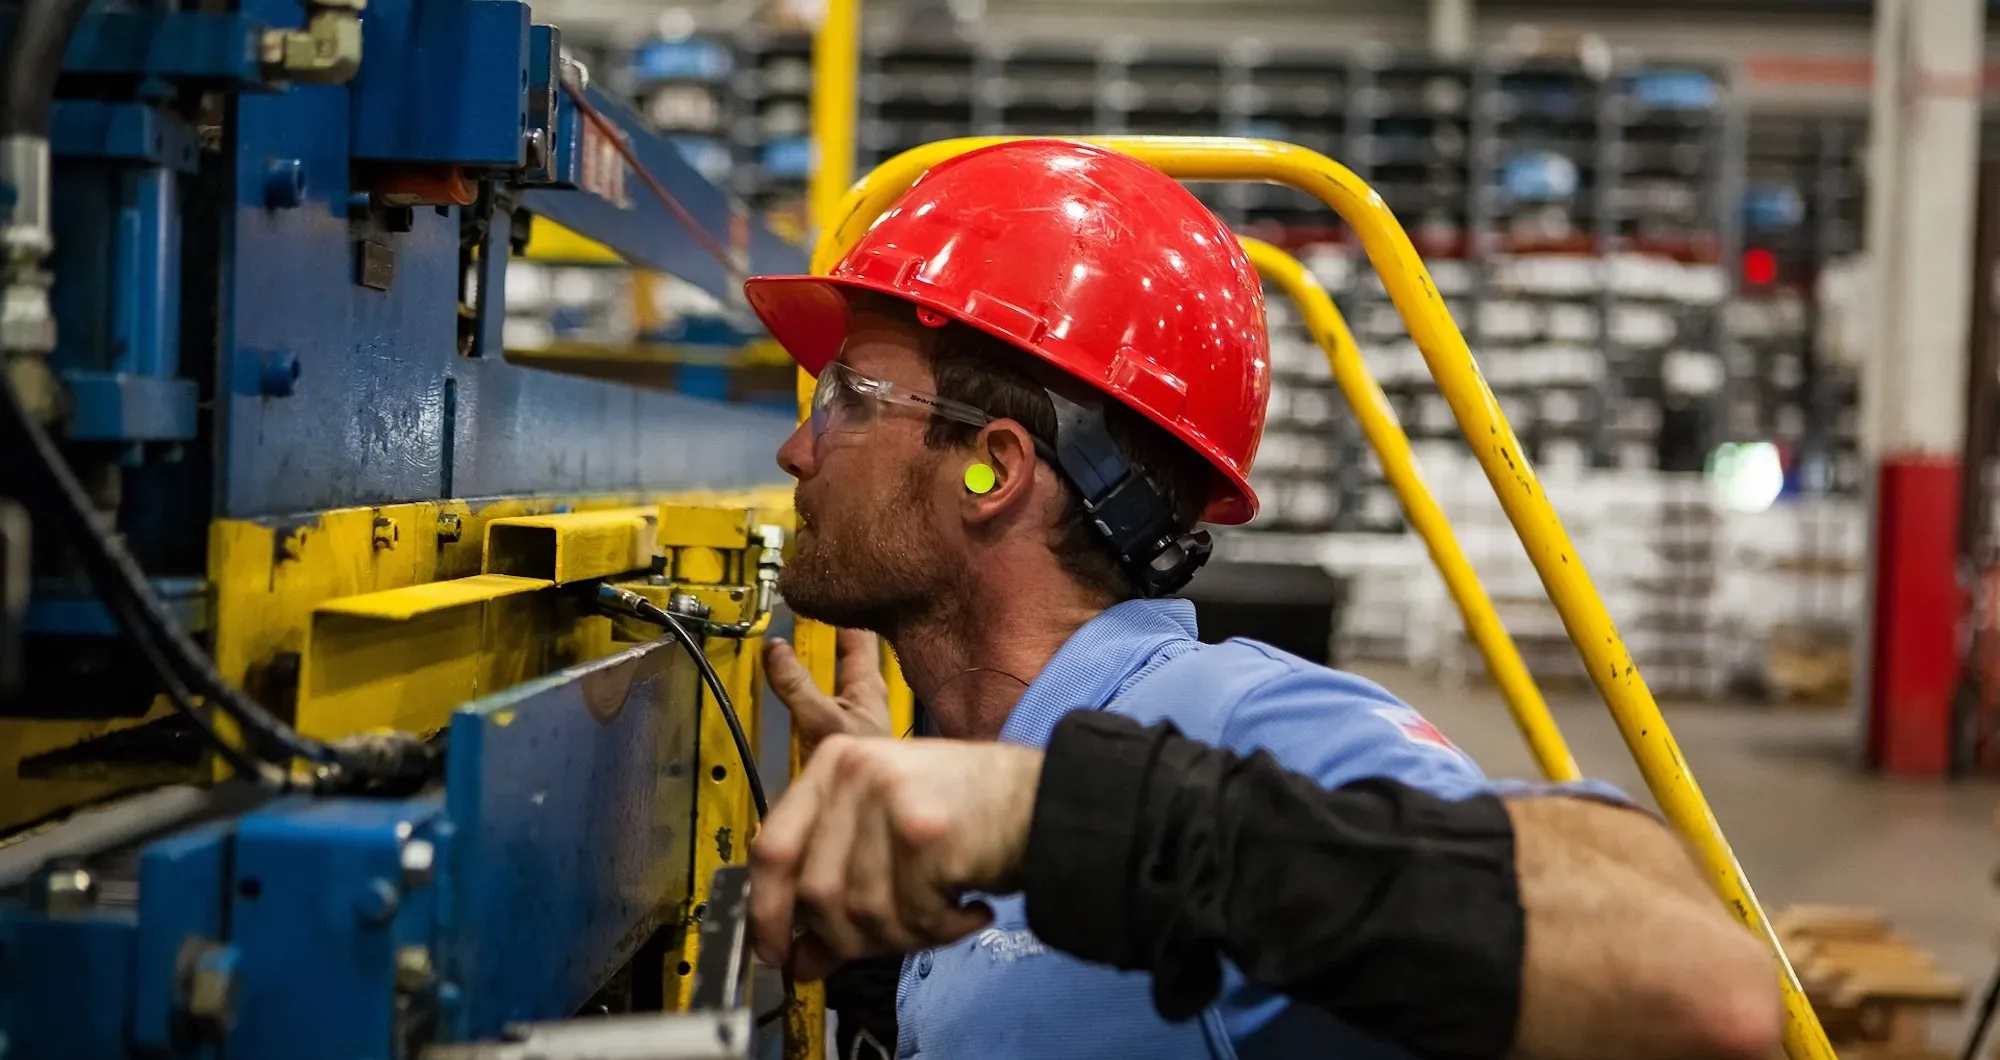
Cameras equipped with AI continuously scan the shop floor, checking if workers are wearing essential safety gear such as helmets, gloves, goggles, and masks.
- Deep Learning Algorithms
The system employs sophisticated deep learning techniques to identify different types of PPE, even in challenging or dimly lit environments, ensuring precise detection.
- Instant Notifications
If a violation is detected, the system promptly notifies supervisors or managers, allowing for quick intervention to avert potential hazards.
Features Designed for Manufacturing Environments
Automated PPE Detection: Monitors compliance throughout the shop floor without requiring manual checks.
Comprehensive Coverage: Oversees a variety of protective equipment, from hard hats to safety shoes, ensuring safety protocols are followed.
Integrated AI Surveillance: Upgrades traditional CCTV systems with AI-driven insights for proactive safety management.
Hazard Identification: Detects unsafe behaviours and conditions, assisting manufacturers in mitigating risks before incidents happen.
Benefits for Manufacturing Facilities
24/7 Safety Compliance: Ongoing monitoring guarantees that safety standards are consistently upheld.
Reduced Accidents and Downtime: Rapid identification and reporting of violations lessen workplace hazards and operational interruptions.
Enhanced Productivity: A secure work environment improves employee morale and efficiency.
Regulatory Confidence: Ensures compliance with safety regulations, safeguarding businesses from fines and legal complications.
Future-Ready Safety Solutions
AI-driven PPE monitoring goes beyond just spotting non-compliance; it aims to establish new standards for industrial safety. As this technology advances, it will merge with predictive analytics, IoT, and robotics to develop fully autonomous safety systems on factory floors.
From monitoring PPE compliance to spotting environmental hazards, AI is paving the way for a safer, smarter future in manufacturing. With reduced risks and improved efficiency, manufacturers can concentrate on their core mission—delivering excellence.
Conclusion
AI-driven PPE monitoring represents a commitment to the safety and well-being of your workforce. By automating safety measures and utilising advanced technology, manufacturers can safeguard workers, comply with regulations, and maintain seamless productivity. At ThirdEye AI, we offer AI-driven PPE monitoring solutions that utilise CCTV surveillance and computer vision technology. Our solutions enable real-time detection of non-compliance, provide instant alerts, and implement proactive safety measures.